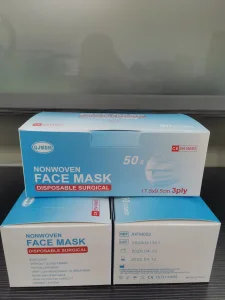
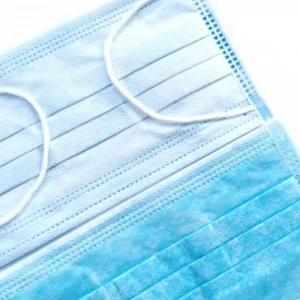
Explore our flagship certified fluid-resistant masks, surgical barriers, and high-efficiency respirators designed for clinical, industrial, and specialized OEM/ODM procurement.

In modern clinical, surgical, and industrial risk environments, fluid-resistant masks serve as the critical primary physical barrier against high-velocity synthetic blood splashes, body fluids, dynamic liquid sprays, and sub-micron bio-aerosols. As an elite OEM/ODM exporter, Henan Tobe Health Co., Ltd. integrates advanced nonwoven material science with precision fluid dynamic resistance engineering.
Engineered to resist synthetic blood penetration under high velocity (80 mmHg, 120 mmHg, and 160 mmHg) per ASTM F1862 and EN 14683 splash resistance standard protocols. Prevents pathogen transmission during arterial spray or high-pressure irrigations.
Features a hydrophobic spunbond outer layer (resists liquid impact), an ultra-fine electrostatically charged meltblown filtration core (captures $\ge 99\%$ bacteria and viral particles), and a hypoallergenic inner contact web designed for zero-skin irritation.
Optimized pore size distribution enables high differential pressure comfort ($\Delta P < 60 \text{ Pa/cm}^2$), balancing maximum fluid imperviousness with superior breathability during prolonged surgical procedures and industrial wear.
Henan Tobe Health Co., Ltd. is a comprehensive medical and health technology enterprise, affiliated with a well-established industrial group. The company integrates research and development, manufacturing, sales, and after-sales service, focusing on protective products, medical devices, medical consumables, and health-related equipment.
The company covers an area of approximately 100 mu, with modern production workshops exceeding 400,000 square meters and a workforce of over 3,000 employees. Its business scope spans multiple sectors including healthcare, medical aesthetics, rehabilitation, and health management services, demonstrating strong industrial integration capabilities.
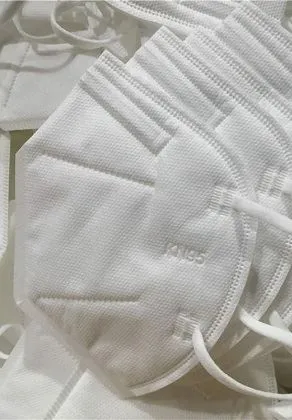
China has established itself as the global epicenter of high-performance technical nonwoven manufacturing and protective medical device production. Leveraging Henan Tobe Health’s centralized manufacturing hub provides unparalleled strategic advantages to international healthcare distributors, brand owners, and emergency relief organizations.
From raw polypropylene resin polymerization to meltblown nonwoven extrusion, electrostatic charging, ultrasonic sealing, and automated packaging, our facility operates within an integrated supply ecosystem. This guarantees raw material consistency, eliminates supply bottleneck risks, and provides dynamic cost efficiency for high-volume B2B contract orders.
Fluid-resistant surgical masks and sterile barriers are manufactured in strictly controlled environmental conditions. Our production environment monitors micro-particulate counts, airborne bio-burden levels, temperature, and humidity, ensuring compliance with international medical device bio-burden standards prior to Ethylene Oxide (EO) sterilization.
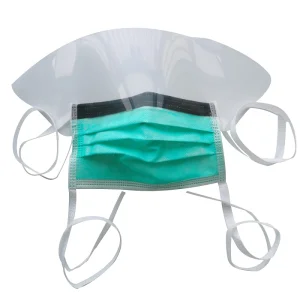
We provide full-spectrum contract manufacturing services: custom dimension tailoring, inner/outer layer GSM weight adjustments, custom logo embossing, anti-fog nose bridge foam application, anti-glare visor/splash shield integration, and private label packaging design (boxes, individual sterile pouches, and bulk master cartons).
Our facility houses an in-house physical & microbiological laboratory equipped with hydrostatic pressure testers, synthetic blood penetration rigs, differential pressure manometers, and automated filter efficiency test benches (TSI 8130A). Being on the Ministry of Commerce Whitelist guarantees flawless customs clearance worldwide.
The global personal protective equipment (PPE) market is transitioning from simple volume sourcing to strict compliance, specialized fluid-resistance functionalization, and sustainable material innovation.
Global hospital systems and healthcare authorities are prioritizing ESG initiatives. Future-ready OEM buyers are increasingly demanding fluid-resistant masks utilizing Polylactic Acid (PLA) nonwovens and recyclable polypropylene blends that maintain hydrostatic performance while reducing medical waste carbon footprints.
Modern clinical surgical environments demand integrated solutions. Our product range incorporates anti-glare optical films, anti-fog nose cushion seals, and optically clear fluid splash shields to protect healthcare personnel against fluid spray and ocular splatter simultaneously.
Global procurement networks require dual-market readiness. Henan Tobe Health aligns manufacturing specifications to conform simultaneously with European Union standard EN 14683 Type IIR and American ASTM F2100 Level 3 specifications, streamlining global inventory distribution.
Scenario: High-risk cardiovascular, orthopedic, and trauma surgeries where arterial bleeding, high-pressure irrigation, and surgical splash hazards are present.
Solution: ASTM F2100 Level 3 / EN14683 Type IIR masks featuring 160 mmHg fluid resistance, anti-fog foam strips to prevent optical fogging of surgeon eyewear, and non-glare integrated eye shields.
Scenario: High-speed dental drills, ultrasonic scalers, and air-water syringes generating continuous fluid aerosols and saliva splatter mixed with potential pathogens.
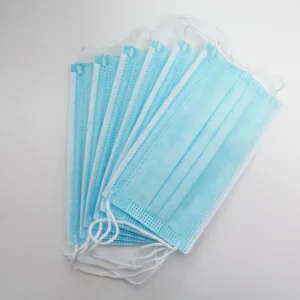
Solution: Hydrophobic 3-ply/4-ply surgical masks with high fluid barrier rating, comfortable soft earloops, and high breathability for prolonged dental treatment sessions.
Scenario: Precision drug compounding, cell culture handling, and chemical fluid processing requiring micro-particle containment and liquid splash mitigation.
Solution: Low-linting, ultra-clean nonwoven masks packaged in cleanroom-compatible double-bagged sterile formats, preventing particulate contamination in controlled environments.
Scenario: Paramedics, epidemic control personnel, and field military medical teams operating in unpredictable, hazardous fluid splash environments.
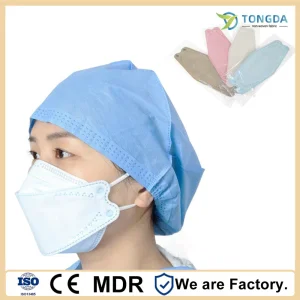
Solution: High-barrier respirator-style protective masks (N95 / FFP2 / KF94) combining multi-layer particulate filtration with fluid-repellent outer shells for rugged field deployment.
Henan Tobe Health Co., Ltd. maintains a extensive medical and protective equipment portfolio backed by internationally recognized quality standard certifications.
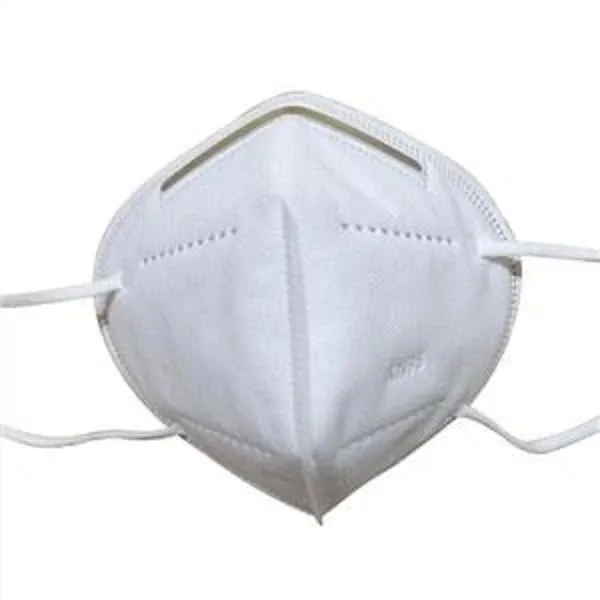
Henan Tobe Health Co., Ltd. has established an advanced R&D center staffed with over 20 experienced engineers and technical experts. The team is dedicated to continuous innovation, product upgrades, and the development of high-barrier nonwoven technologies.
Utilizing state-of-the-art automated production lines and precision testing equipment, combined with internationally advanced manufacturing management systems, our company operates over 20 automated mask production lines to ensure stable supply capacity and consistent product quality.
Supported by a professional international sales and service team, we offer global enterprise clients:
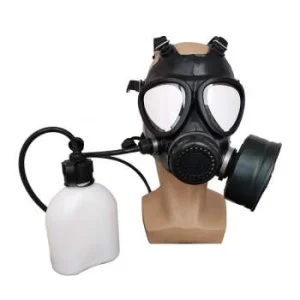
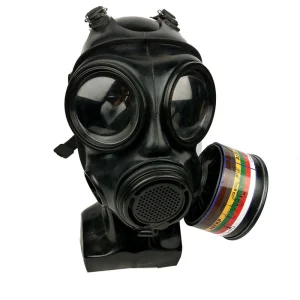
Discover our specialized protective lineup including splash-shield surgical masks, active carbon filters, gas masks, and full-face medical protective gear.
Technical, regulatory, and procurement insights for international distributors, medical purchasing managers, and brand partners.
Customer-oriented, driven by innovation, Henan Tobe Health Co., Ltd. is committed to promoting advanced medical technologies, enhancing end-user service value, and contributing to the global healthcare industry.
To become a leading high-tech enterprise with core technologies and integrated system solutions in the medical and health industry, making significant contributions to the advancement of medical equipment and global health services.
To integrate science and technology into healthcare and improve the quality of human life through continuous innovation, industrial precision, and absolute product reliability.
 Tobe Health